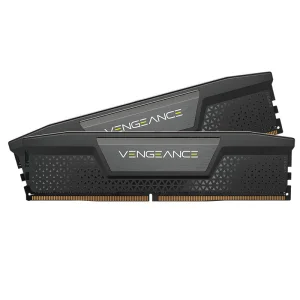
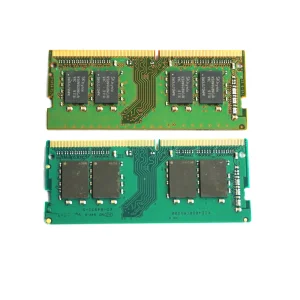
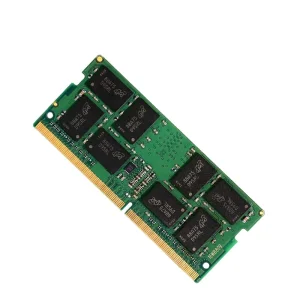
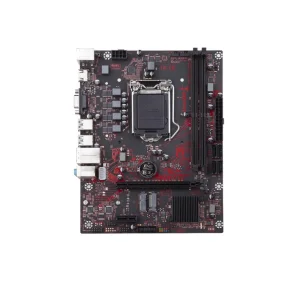
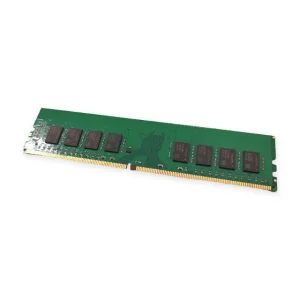
Discover our elite line of high-speed memory modules, server components, and enterprise-grade hardware engineered to power high-throughput routers and edge computing systems.
Founded in 2016, Kryntel Memory Technology (China) Co., Ltd. stands as an elite professional manufacturer specializing in high-performance RAM modules and robust network hardware infrastructure for global OEM, ODM, and private label partners. Operating from a state-of-the-art facility covering approximately 320㎡, we focus relentlessly on delivering stable, ultra-fast, and energy-efficient digital solutions tailored for advanced networking, gaming, industrial automation, and enterprise server applications.
As the global economy accelerates its digital transformation, reliable, high-speed, and secure wireless communication is no longer a luxury—it is the operational backbone of modern enterprises. CE Certified WiFi Routers and networking hardware dictate how modern supply chains, smart cities, and industrial IoT (IIoT) ecosystems synchronize data.
Smart factories demand uninterrupted low-latency wireless communication. Our CE certified routing and hardware solutions empower automated manufacturing lines, robotics coordination, and real-time telemetry tracking.
Municipal networks require robust hardware capable of withstanding extreme outdoor environments while processing high-density data traffic from traffic management, public safety, and utility grids.
Enterprise networks rely on hardware-backed encryption and stable high-frequency memory to safeguard sensitive corporate assets against evolving cyber threats and unauthorized data interception.
International trade compliance requires rigorous adherence to safety, electromagnetic compatibility (EMC), and environmental directives. Our export-grade WiFi routing equipment and memory modules proudly carry CE, FCC, and RoHS certifications, assuring seamless customs clearance and deployment across North America, Europe, the Middle East, and Southeast Asia.
Our quality control regime spans incoming raw material verification, rigorous in-process quality monitoring, extended thermal aging stress tests, and stringent final pre-shipment sampling.
We execute extensive compatibility testing against leading motherboard architectures, high-bandwidth stress testing, and precise voltage stability checks under fluctuating thermal loads.
Backed by experienced export teams familiar with regional regulatory frameworks, we provide frictionless logistics to major markets including the US, Germany, India, Brazil, and the UAE.
Innovation drives market leadership. In the past fiscal year alone, our dedicated R&D department of approximately 160 elite engineers successfully engineered and launched over 280 advanced memory and networking hardware products across DDR4 and DDR5 series.
Pushing bandwidth boundaries up to 6000MHz and beyond, optimizing data throughput for heavy computing workloads.
Advanced copper-aluminum composite heatsinks and passive cooling designs ensuring prolonged hardware lifespan.
Tailored frequency tuning, latency adjustments, and specialized PCB architecture optimization for OEM/ODM partners.
Eco-conscious power management integrated into every circuit design to minimize thermal dissipation and power draw.
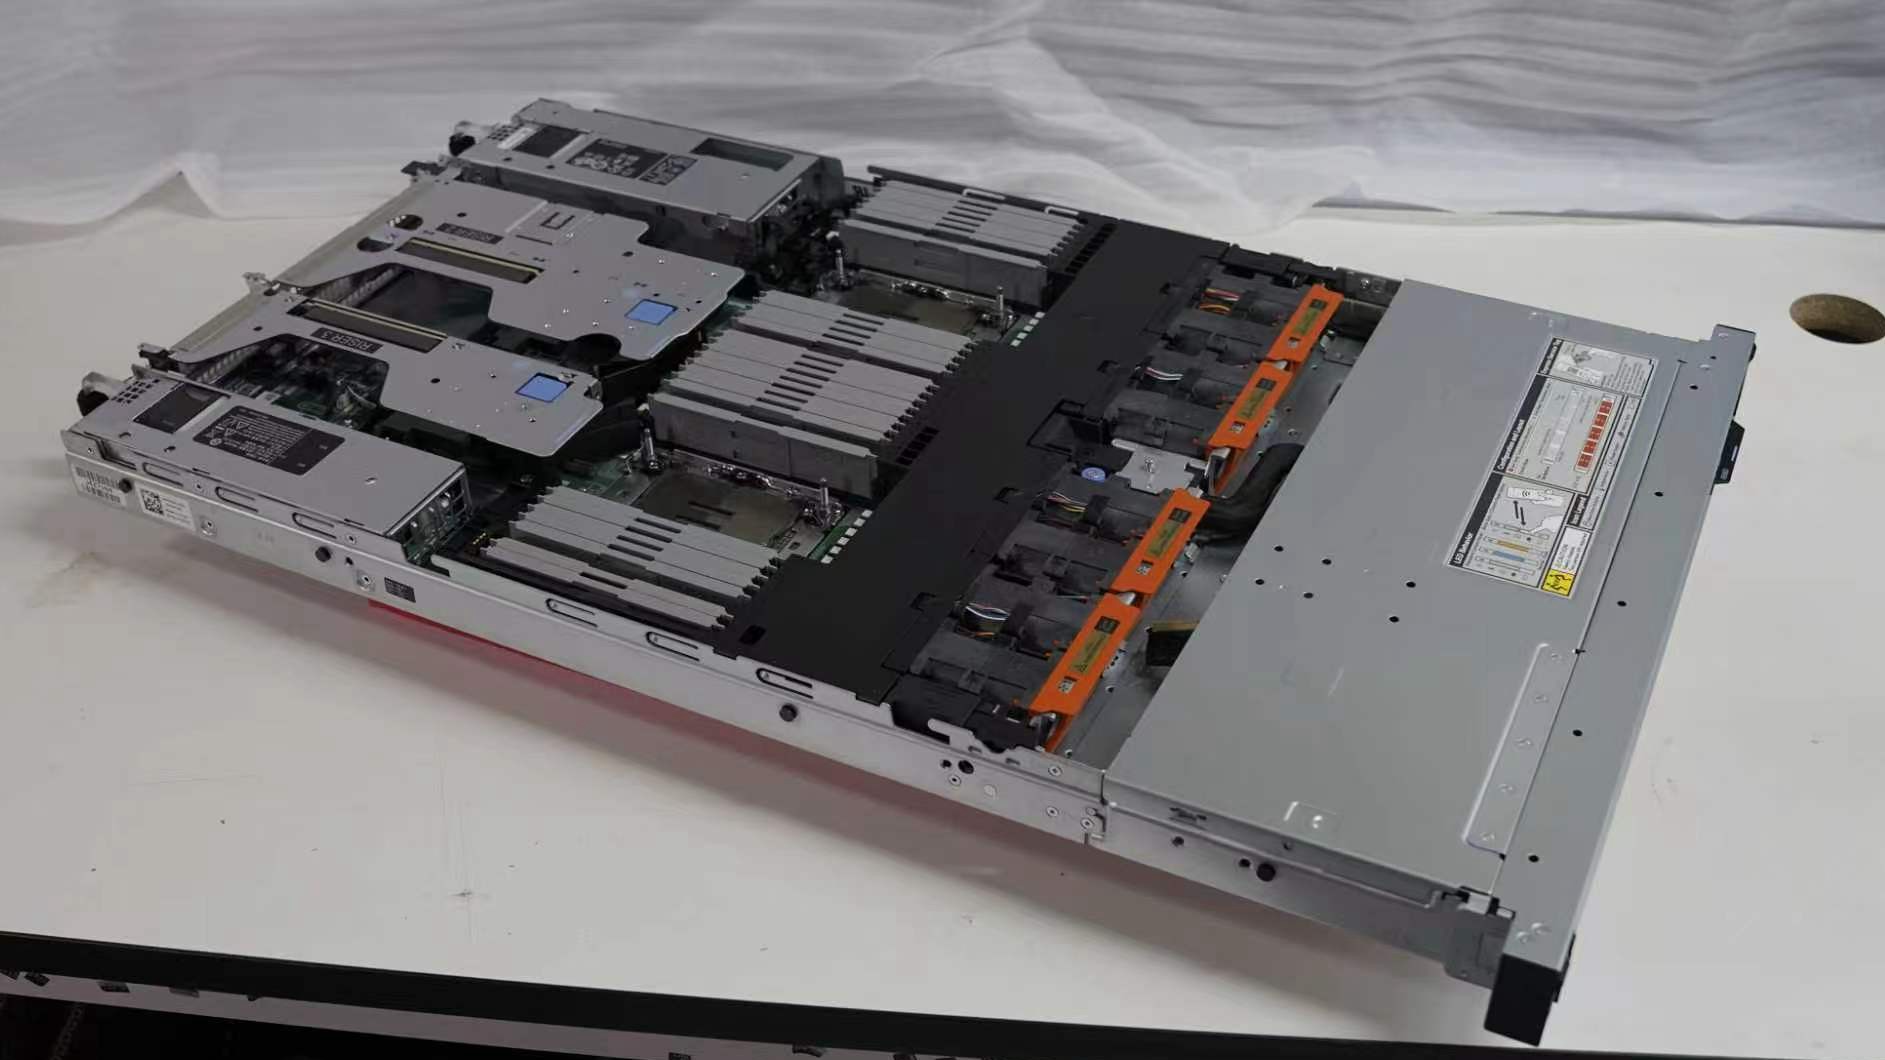
Explore our comprehensive inventory of specialized server motherboards, cooling systems, and high-speed memory modules designed to support robust wireless communication networks.
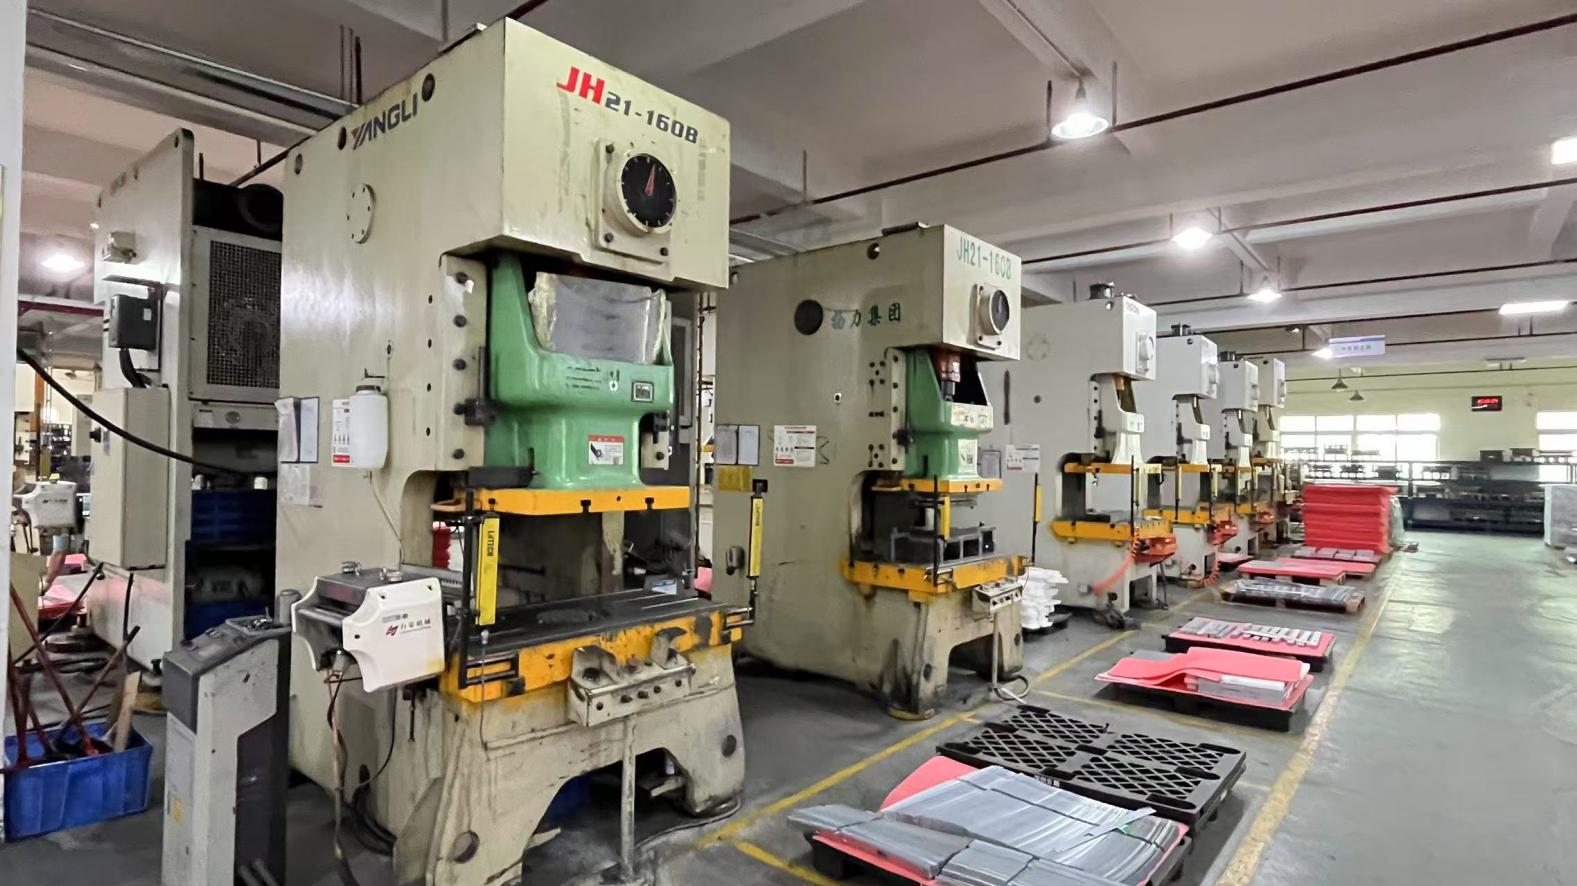
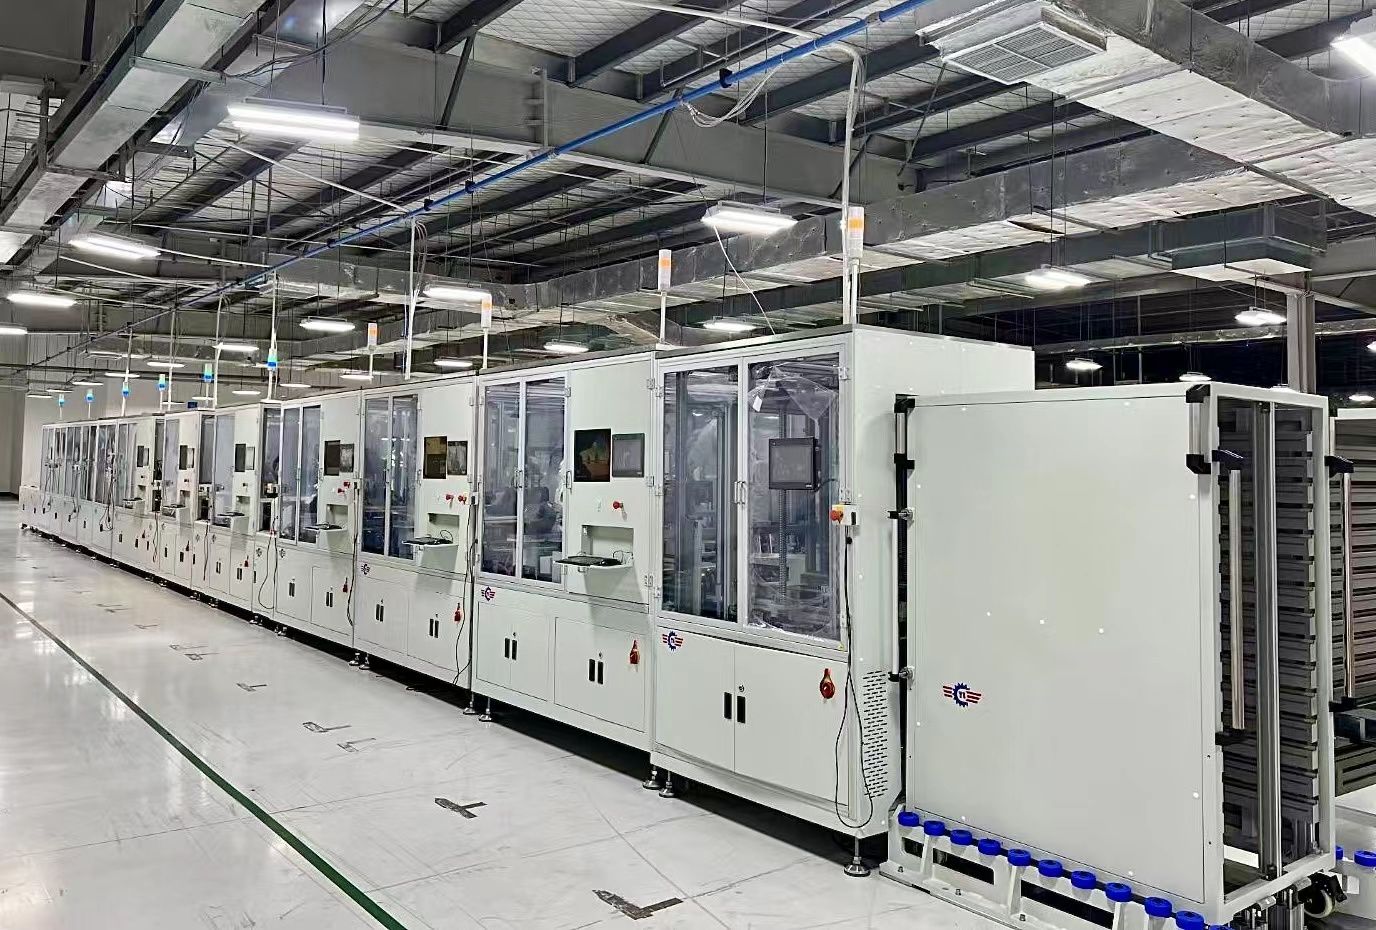
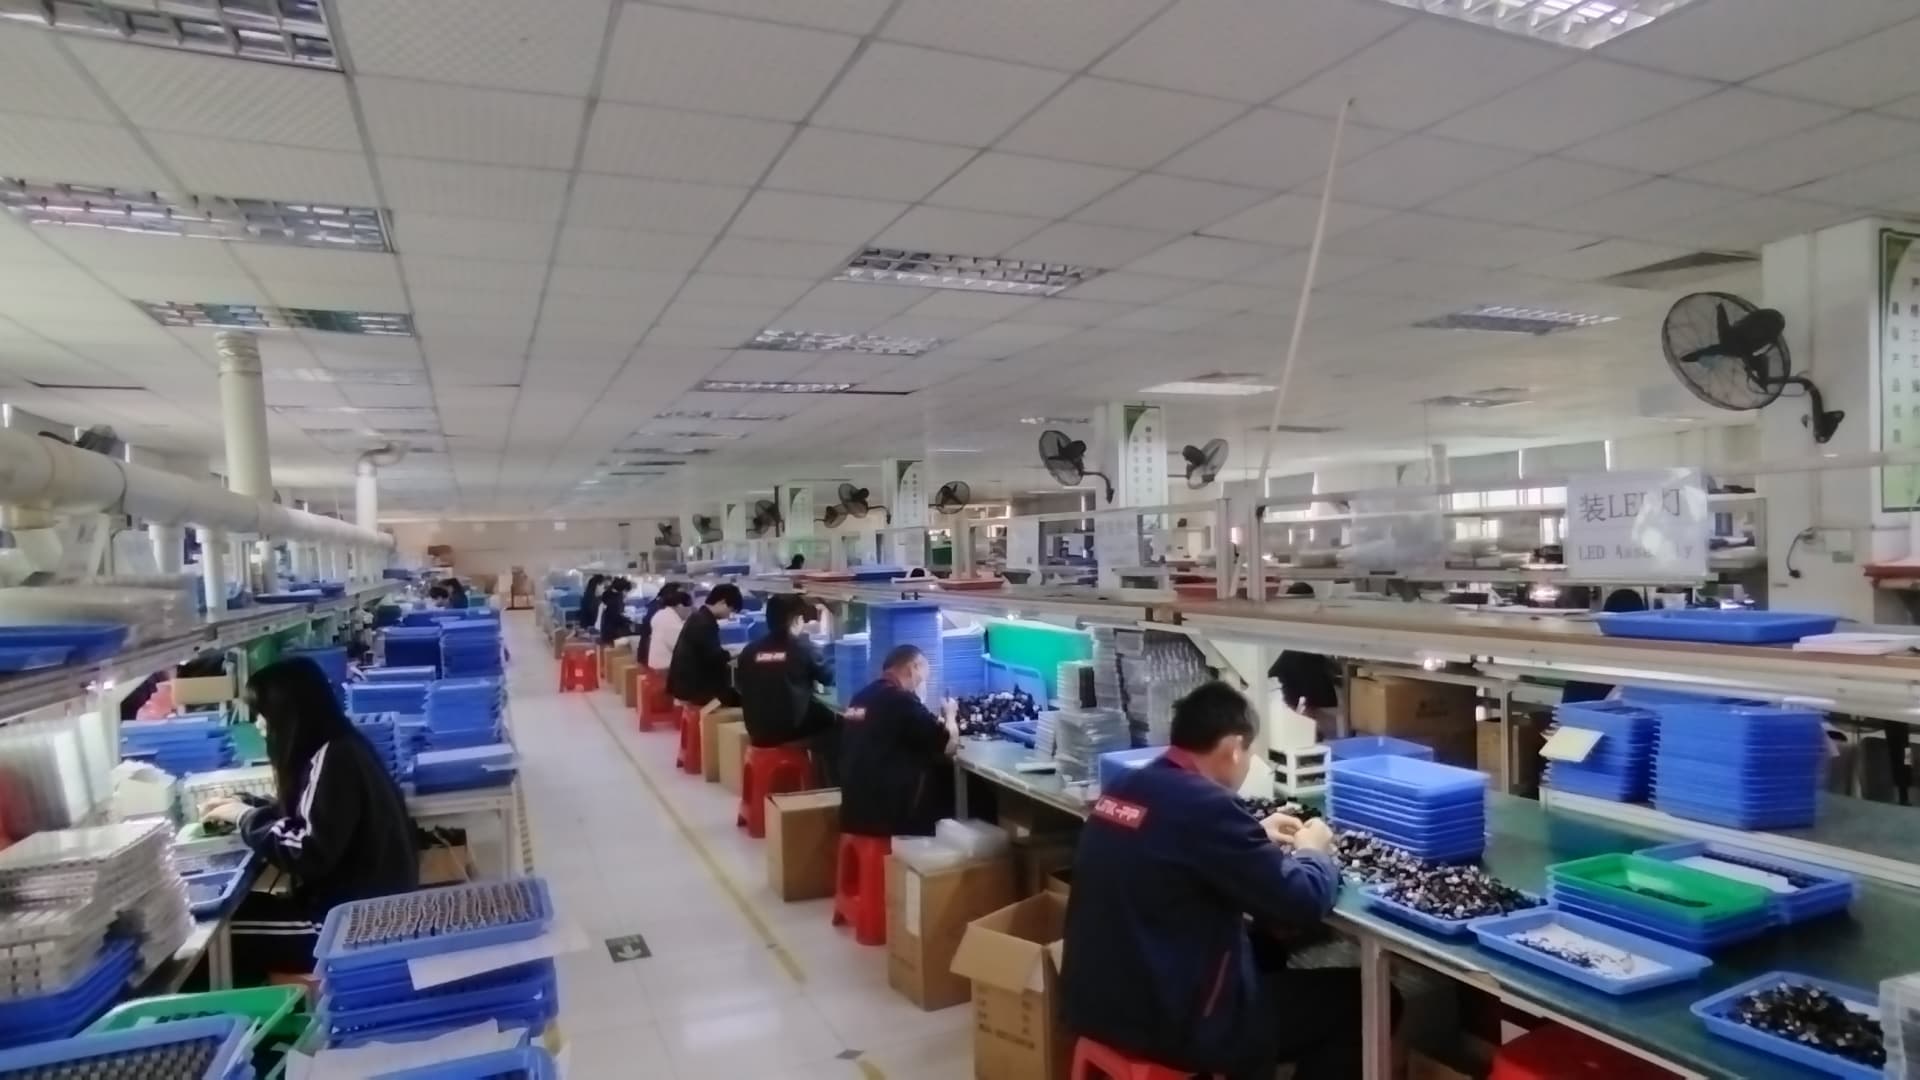
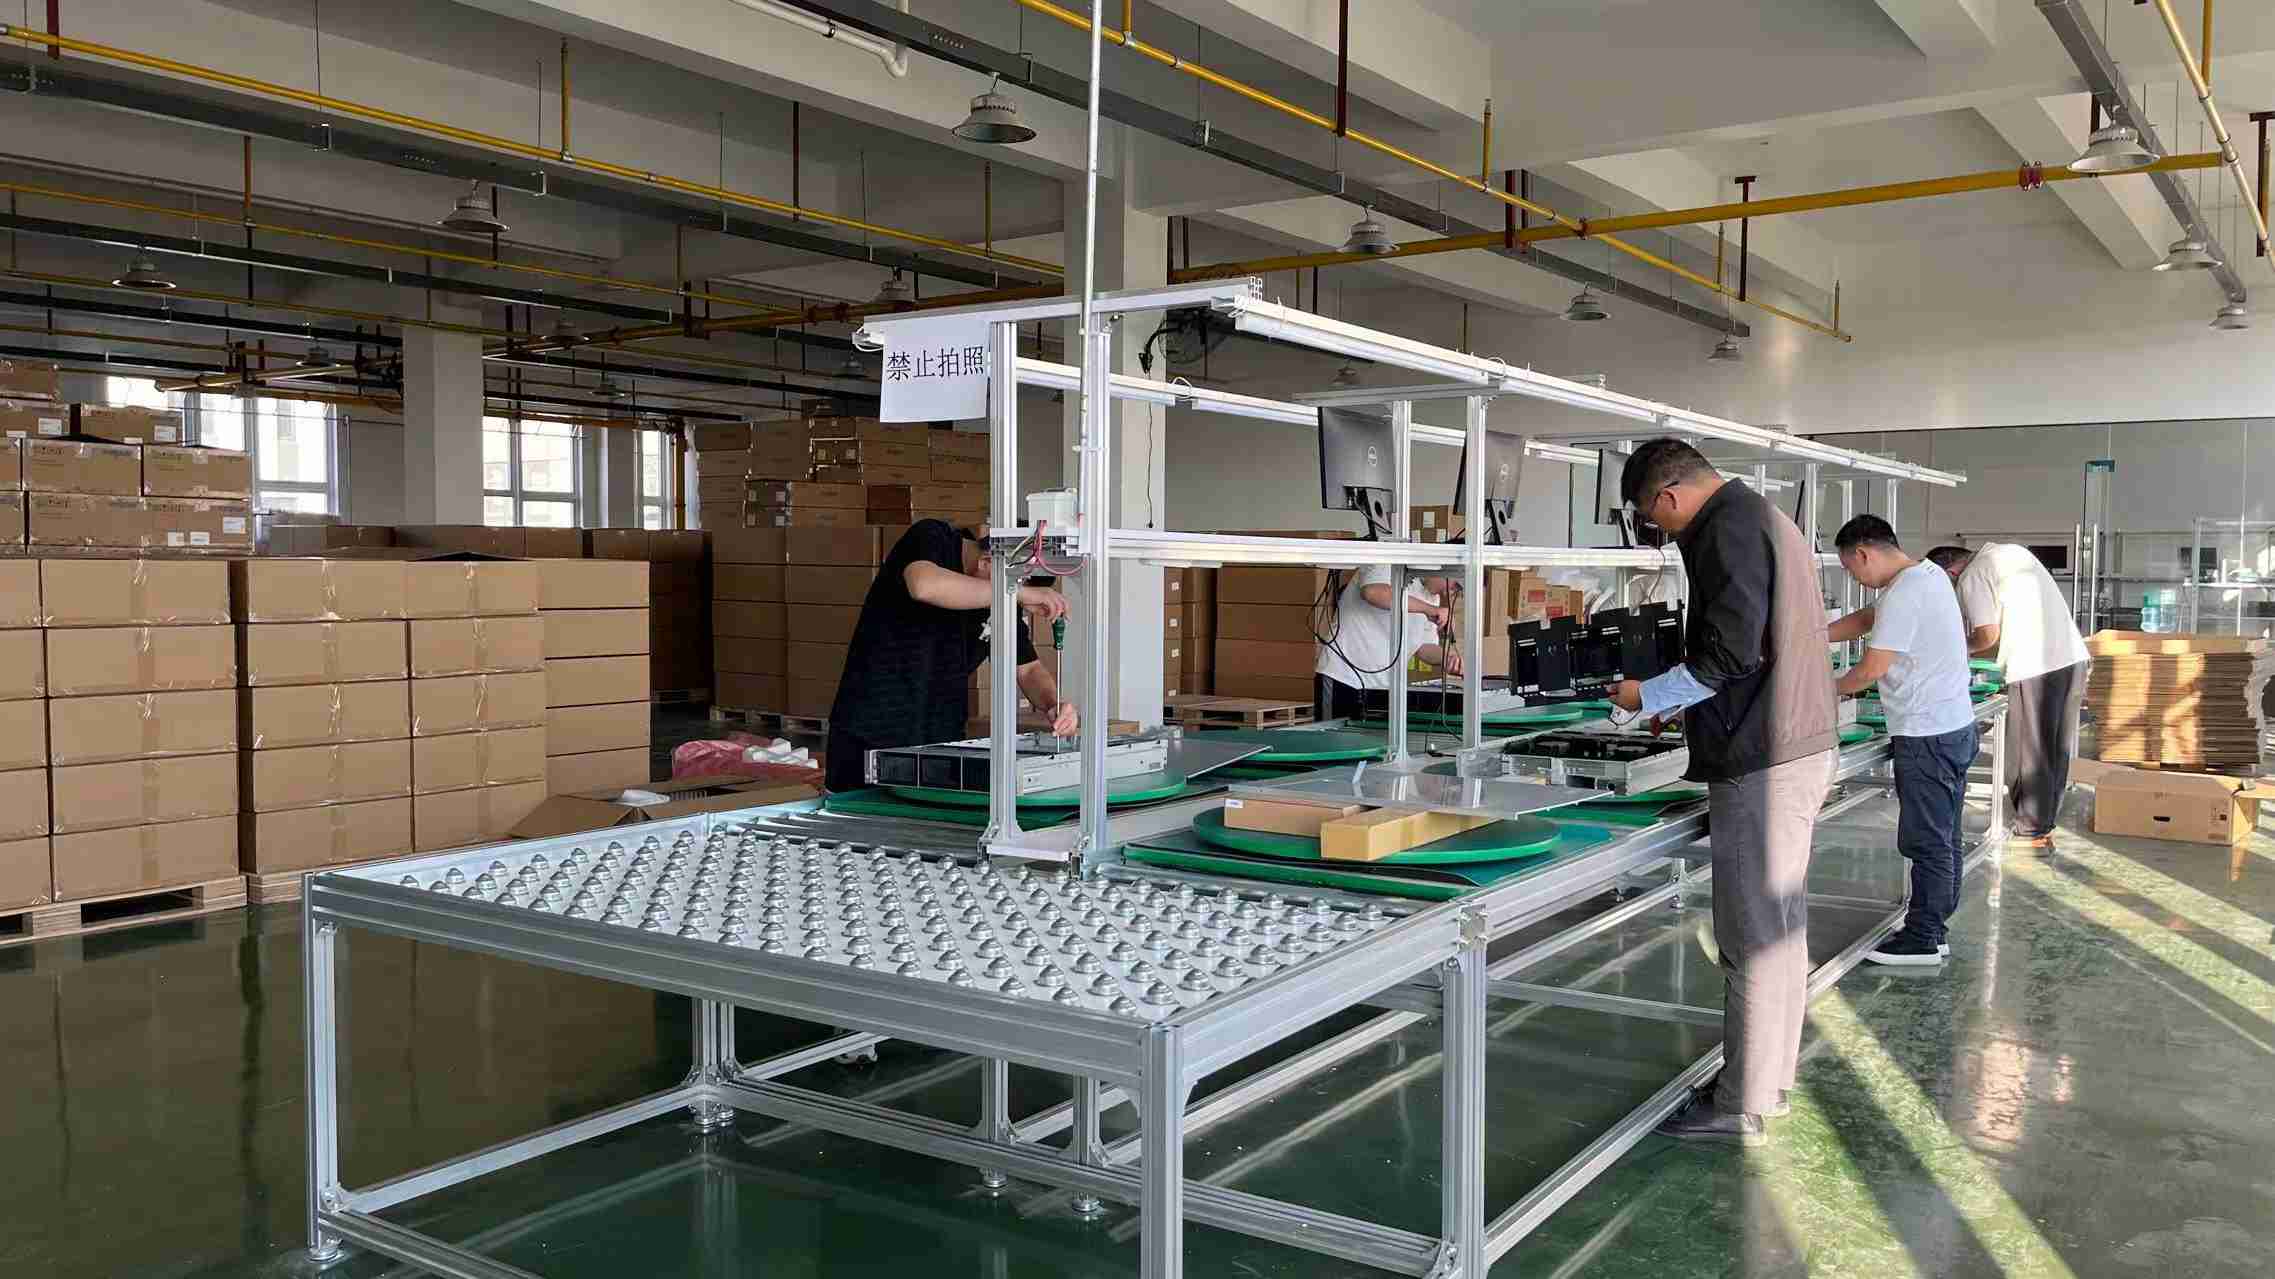
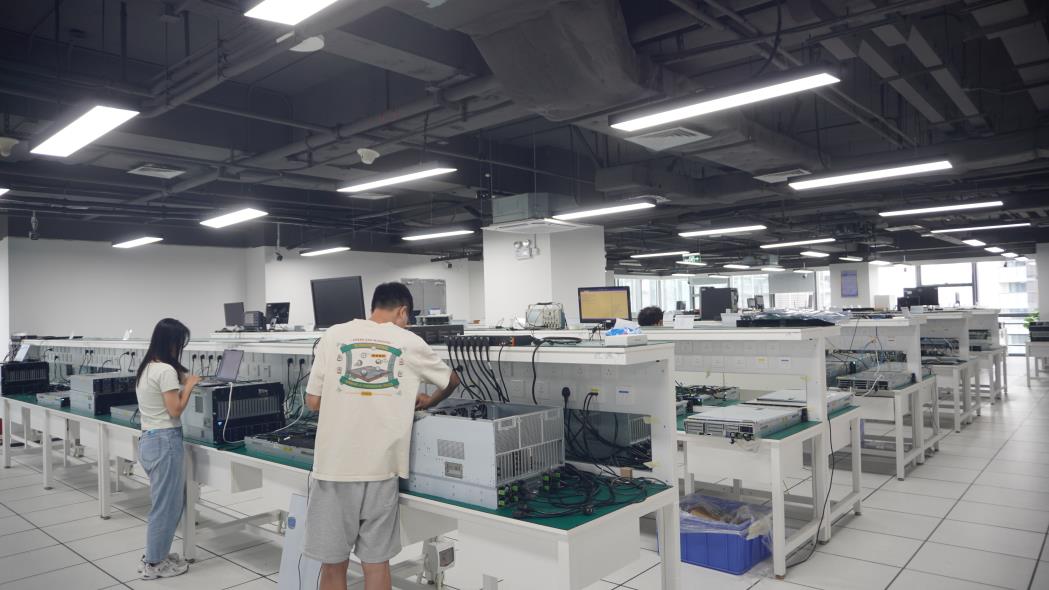
A visual tour of our advanced production lines, testing laboratories, and engineering facilities that ensure world-class quality for every product exported globally.
Expert answers regarding our CE certified networking hardware, OEM/ODM capabilities, and global export processes.
Our products are fully compliant with major international standards, holding CE, FCC, and RoHS certifications, ensuring smooth legal entry and deployment across European, North American, and global markets.
Yes. We offer complete OEM/ODM solutions including PCB layout optimization, customized branding, heat spreader design, firmware tuning, and specialized packaging tailored to private label partners.
Backed by a robust supply chain network of over 1,200 upstream partners and extensive inventory, standard orders are processed and shipped efficiently to meet urgent global commercial demands.
We employ a dedicated team of 42 QA professionals executing multi-stage inspections, high-temperature aging tests, motherboard platform compatibility checks, and rigorous voltage stability analysis.
 Kryntel